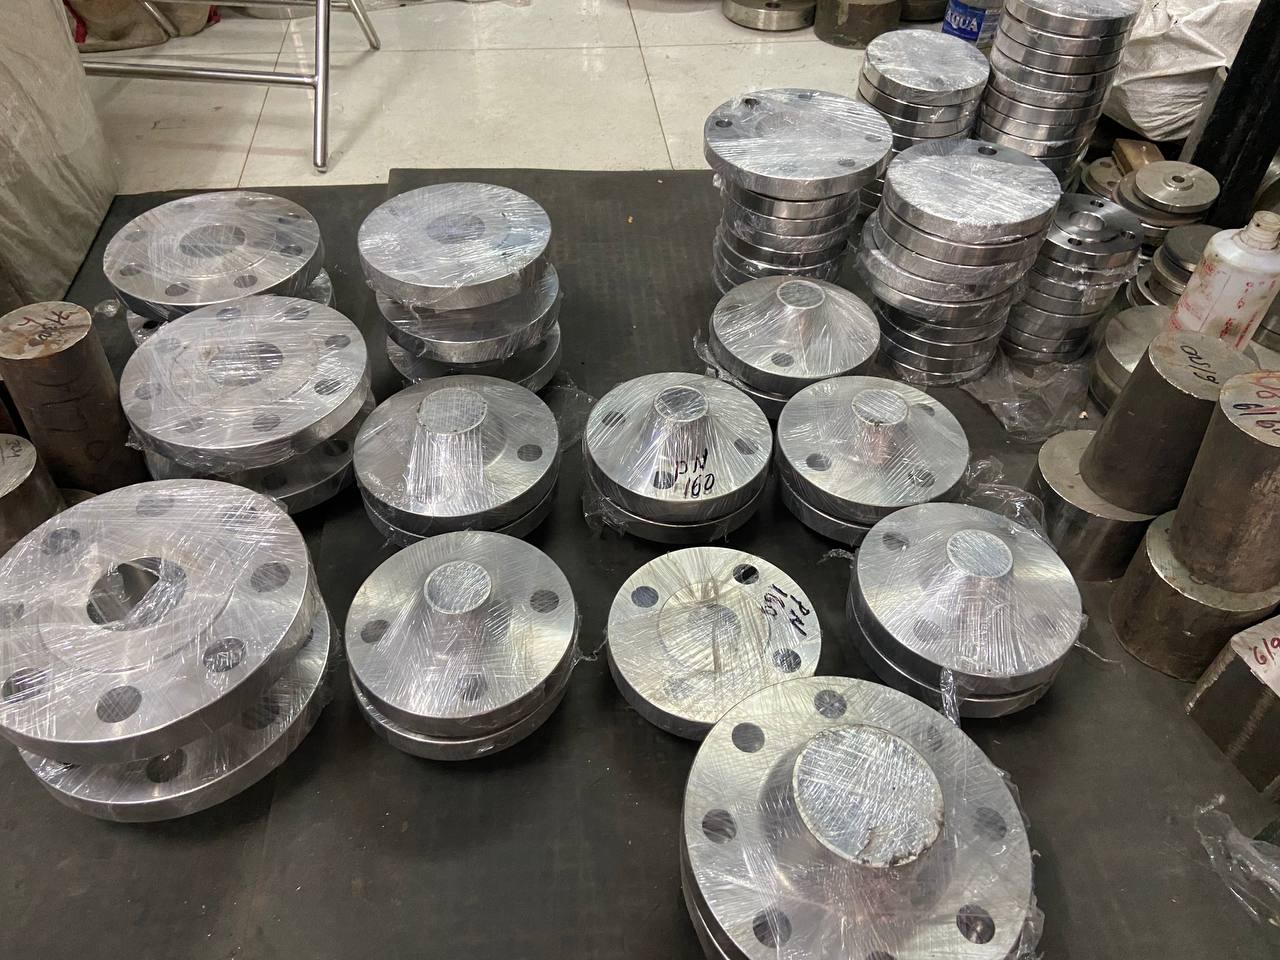
Tesco Steel & Engineering manufactures ASTM A182 F304 lap joint flanges — the page where the lap joint bench opens its austenitic wing, on the grade the pattern's alloy economy was practically written for: the 18/8 classic (UNS S30400, W.Nr. 1.4301), chromium 18–20% and nickel 8–11% with nothing else added — no molybdenum; that is 316's addition. On a 304 line the stainless stub end wets and the ring is chosen by the site: the economy's carbon steel ring via our A105 page, or this page's stainless answer — washdown plants, coastal air, and cryogenic duty where austenite's toughness simply continues, no Charpy required. The certificate is the austenitic signature: 515/205 MPa at 30% elongation, solution annealed, dual-certified 304/304L where the heat qualifies. The ring never welds; the single butt weld belongs to the A403 WP304 stub end per B16.9. Per ASME B16.5, ½″–24″ NB, Classes 150–2500, pickled & passivated. Every lot with EN 10204 3.1/3.2 MTC. ISO 9001:2015, made in Mumbai, India — exported to 50+ countries.
ASTM A182 F304 · UNS S30400 · W.Nr. 1.4301The 18/8 Austenitic ClassicThe Economy's Original GradeCryo Toughness — No Charpy RequiredDual 304/304L CertificationStub Ends: A403 WP304 per B16.9½″–24″ NB · Classes 150–2500EN 10204 3.1 / 3.2 · ISO 9001:2015
ASTM A182 F304 Lap Joint Flanges — Specifications at a Glance
What is an ASTM A182 F304 Lap Joint Flange?
The classic's backing flange. An ASTM A182 F304 lap joint flange is the loose backing ring of the two-piece system in the 18/8 austenitic classic (UNS S30400) — the world's default stainless, with no molybdenum (316's addition) and no exotic alloying. The point on this pattern: the stainless stub end wets the line, and the ring is chosen by the site — the economy's carbon steel ring, or this page's stainless answer for washdown plants, coastal air and cryogenic cold, where austenite's toughness needs no impact certificate. Per ASME B16.5, ½″–24″ NB, Classes 150–2500, solution annealed, 515/205/30%, dual-certified 304/304L; stub ends A403 WP304 per B16.9. EN 10204 3.1 on every lot.
Also searched as: F304 backing flange, 304 stainless lap joint flange, S30400 lap joint flange, 304 loose flange, SS 304 LJ flange — all this page's product. Related pages: the lap joint hub (the pattern's full story), the economy's cheap half — A105 — the chloride ladder upward — F316L and F51 duplex — the family variants F304L and F304H — the F304 bench — weld neck / blind / long weld neck — and the stainless steel overview.
The Two Honest Answers — What Backs a 304 Line
The Site
The Wetted Half
The Backing Flange
Indoor process lines, utility duty — the textbook order
A403 WP304 stub end
Plain or galvanised A105 — the pattern's original economy, at a fraction of solid-stainless cost
Washdown & hygienic plants, coastal air, cryogenic systems (this page)
A403 WP304 stub end
F304 — stainless through the joint: nothing sheds, nothing stains, nothing turns brittle
This is the bench's original story: the alloy economy was practically invented for austenitic lines — and the stainless answer wins where the ring's own life argues for it: constant washdown, salt air, or the cold that climbs the line. Both halves are quoted from this site either way.
F304 on the Chloride Ladder
Rung
Grade
What the Money Buys
The austenitic base (this page)
F304 — 18/8, no molybdenum
General corrosion, hygienic service and cryogenic cold — the economical default
PREN ≥40 — hot seawater and aggressive brines, at 550 MPa yield
The honest advice starts at the bottom: duty without meaningful chlorides gains nothing from paying for molybdenum — and duty with them steps up the ladder, one named reason at a time.
What the Pattern Gives This Grade
The Original Economy
The alloy economy was practically written for 304 lines — the stainless stub end wets, the ring follows the site's choice, and the gap between the two answers is smaller here than anywhere on the alloy bench.
The Cryo Answer Without Paperwork
The never-wetted ring still gets cold — and austenite cannot turn brittle: no test temperature, no per-lot Charpy certificates, where the carbon ladder's rings need both. On cryogenic lap joints this often settles the ring question alone.
The Sensitization Immunity
A ring no weld ever touches cannot sensitize — the L-grade question belongs entirely to the stub end's butt weld, where dual 304/304L certification answers it.
The Rotation, Weekly
Hygienic pipework is broken and remade constantly — and a loose ring that rotates to align bolt holes is the pattern's oldest virtue, earning its keep at every washdown teardown.
Specification Notes — Getting F304 Lap Joints Right
Three honest notes.Chlorides change the grade: 304 has no molybdenum — saline, brackish or chlorinated duty reads 316L and the ladder above it, and coastal process duty is a different question from coastal air. The yield is the bench's gentlest: 205 MPa sizes high-class rings honestly, and the austenitic group's B16.5 ratings derate faster with temperature than carbon steel's — the class tables govern. And the pattern's boundaries apply in any grade: heavy external loads, severe vibration and high-moment positions read the weld neck bench — lap joints earn their place where lines dismantle; the hub page states the boundaries fully.
How Our F304 Lap Joint Flanges Are Manufactured
1
Material — certified A182 F304 forgings, solution annealed and quenched, furnace records retained; heat-number transfer at the first operation.
2
Machining — B16.5 lap joint dimensions: OD, thickness, bolt circle to class; bore and shoulder turned to suit the stub end's lap — 304's work-hardening makes this tougher than the numbers suggest, a problem we own so you don't.
3
Shoulder dressing — the radius dressed to bear evenly on the back of the lap — spreading bolt load instead of concentrating it.
4
Testing — chemistry certified per heat, dual 304/304L designations stated where the heat qualifies; PMI on the Cr-Ni signature.
5
Pickling & passivation — stainless's own finish, restoring the passive film — never painted, never galvanised; and no welding, ever — a ring no weld touches cannot sensitize.
6
Pairing & certification — matched to A403 WP304 stub ends where ordered; one EN 10204 3.1 document per pair (3.2 witnessed on request); packed sea-worthy with laps and shoulders protected.
Where F304 Lap Joint Flanges Are Used
Where the classic and the pattern meet: food, dairy, beverage and pharmaceutical plants whose pipework dismantles for cleaning on schedule — the lap joint's oldest hygienic franchise — water treatment and general chemical duty inside 304's chloride limits, cryogenic systems from LNG utilities to liquid-nitrogen and CO2 service where austenite simply continues, and the everyday process lines where the economy answer backs a WP304 stub end with carbon steel. Production and supply below:
Stainless Lap Joints with Stub Ends — The Two-Piece PairThe Two-Piece System — Flange, Stub End, Butt Weld, PipeF304 Production — Machining at Our Works
F304 Lap Joint Flange Dimensions
Flange dimensions are class-governed per ASME B16.5 — identical in every grade; stub ends per B16.9. Full class-by-class charts:
Example: “Lap Joint Flange, 4″ NB, ASME B16.5 Class 150, ASTM A182 F304 dual-certified 304/304L, with A403 WP304 stub ends Sch 40S (B16.9 Type A, supplied together), pairs on one MTC, EN 10204 3.1 — 30 sets.” Quotations normally within 24 hours with price, unit weights (both parts) and delivery.
F304 Lap Joint Flanges — Frequently Asked Questions
What is an ASTM A182 F304 lap joint flange?
An ASTM A182 F304 lap joint flange is the loose backing flange of the two-piece lap joint system, forged in the 18/8 austenitic classic (UNS S30400, W.Nr. 1.4301) — the world's default stainless steel, carrying general corrosion duty, hygienic service and cryogenic cold on the same certificate. Like every lap joint flange it slides over the pipe, sits free behind the stub end's flared lap, and carries the entire bolt load without touching the line fluid. This is the grade the pattern's famous alloy economy was practically written for — the stainless stub end wets the line while the ring is chosen by the site, as the FAQs below explain — and where the site chooses stainless, this page's product is the answer. Manufactured per ASME B16.5 in ½" to 24" NB, Classes 150 to 2500, solution annealed, pickled and passivated, dual-certified 304/304L where the heat qualifies, with EN 10204 3.1/3.2 on every lot.
How does the two-piece lap joint system work?
By splitting sealing from bolting. The stub end butt-welds to the pipe: its flared lap provides the gasket face and does all the fluid contact. The backing flange never welds and never wets: it slides on before the stub end is welded — the classic site lesson — spins freely until the bolts enter, and transmits bolt load through its radiused shoulder onto the back of the lap. Two virtues follow, and 304 lines enjoy both at full strength: bolt holes always align, because the loose ring rotates — beloved wherever hygienic pipework is broken and remade weekly — and the flange's material follows its own duty rather than the line's chemistry, which is the alloy economy the next FAQ weighs. The full pattern story — stub end types, the economy, the honest boundaries — is on the lap joint hub page.
Does the backing flange behind a 304 line need to be stainless — the two honest answers?
It depends on the site, and both answers are honest. The economy answer — the pattern's original story: the ring never touches the process, so a plain or galvanised carbon steel ring from our A105 page backs the wetted 304 stub end at a fraction of solid-stainless cost; on indoor process lines and utility duty this is the textbook lap joint order, and it is why the pattern exists on stainless systems at all. The stainless answer — this page's product — wins on three kinds of site: washdown and hygienic plants (food, dairy, pharma), where painted or zinc-coated rings shed and stain under constant cleaning and inspection culture wants stainless everything; coastal and chemically humid atmospheres, where the ring's own surface must resist the air it lives in; and cryogenic systems, where the never-wetted ring still gets cold and austenite's toughness needs no impact certificate. State which answer your specification takes and we quote that ring — or both options priced side by side.
What is the chemical composition of ASTM A182 F304 (UNS S30400)?
Carbon ≤0.08%, manganese ≤2.00%, silicon ≤1.00%, chromium 18.0-20.0%, nickel 8.0-11.0%, phosphorus ≤0.045%, sulphur ≤0.030%. Note what is absent: no molybdenum — that is 316's addition for chloride pitting — and no nitrogen floor or deliberate alloying beyond the classic pair. The 0.08% carbon ceiling is the plain grade's; the L-grade halves it to 0.030% for as-welded corrosion duty, and the H-grade sets a floor for creep strength — both covered in their own FAQs below. Chemistry is verified per heat and travels on the EN 10204 3.1 MTC, with dual 304/304L certification stated where the heat qualifies.
What are the mechanical properties of F304 lap joint flanges?
In the solution-annealed condition A182 requires tensile strength 515 MPa (75 ksi) minimum, yield strength 205 MPa (30 ksi) minimum and elongation 30% minimum — the austenitic signature: modest yield, enormous ductility, and toughness that never disappears at low temperature. Two honest notes for the backing-flange duty: this is the gentlest yield on the lap joint bench — the duplex rings double it — so high-class, large-bore joints size their rings accordingly, and B16.5 pressure-temperature ratings for the austenitic group derate faster with temperature than carbon steel's: the class tables, not the yield number, govern the joint's duty. Work-hardening is the flip side: 304 machines tougher than its numbers suggest, which is a manufacturing problem we own so you don't. Supplied with the solution-anneal records retained.
F304 or F304L — and what does dual certification mean?
The L is insurance against weld sensitization. When plain 304 lingers between roughly 450 and 850°C — as a weld heat-affected zone briefly does — chromium carbides precipitate at grain boundaries and locally strip the film, setting up intergranular corrosion in aggressive service. 304L's 0.030% carbon ceiling starves that mechanism, making the L-grade the standard for as-welded corrosion duty. The practical modern answer is dual certification: most mill product is melted with low carbon but still meets plain 304's strength floor, so one heat certifies as both — and our flanges are quoted dual 304/304L where the heat qualifies, satisfying specifications written either way. The lap joint wrinkle is worth savouring: the backing ring is never welded, so sensitization cannot touch it — the L question belongs entirely to the stub end and its butt weld, which is exactly where the dual certificate answers it.
What about F304H for high temperature?
The H-grade runs the carbon logic the other way. Where 304L trims carbon for corrosion, 304H (UNS S30409) specifies it with a floor — 0.04-0.10% — because at creep temperatures carbon is strength: the carbides that sensitize a weld zone are the same phase that pins grain boundaries against slow deformation above roughly 525°C. Refinery hot circuits, steam service and furnace-adjacent duty in the austenitic world therefore name 304H, often with a grain-size requirement attached. On the lap joint bench the H-grade is a rarer request — hot creep duty tends to be welded weld-neck territory, per the pattern's own boundaries — but where a dismantling hot line specifies it, the same two-piece logic applies and the certificate carries the carbon floor. If your specification says 304H, say so on the enquiry: it is a different certificate from the dual 304/304L stock answer, quoted with its own paperwork.
Is F304 suitable for cryogenic service — and does the ring care?
Yes — this is one of austenitic stainless's quiet superpowers, and the ring cares more than you might think. The face-centred-cubic structure has no ductile-brittle transition, so 304 keeps its toughness to liquid-nitrogen temperatures and beyond without the impact-testing gymnastics the carbon steel ladder needs: where A105 stops at -29°C and LF2 at -46°C, austenitic stainless simply continues — LNG, liquid oxygen, liquid nitrogen and CO2 services run on it. Now recall the LF2 page's ambient argument: the backing ring never gets wet, but it does get cold — chilled through the lap it clamps and by the frost climbing the line. A 304 ring answers that argument without a single Charpy specimen: no test temperature to specify, no per-lot impact certificates to file, just a structure that cannot turn brittle. On cryogenic lap joints that is often the whole reason the stainless answer wins over the economy's carbon steel ring.
What stub ends pair with F304 lap joint flanges?
The matching stub end is wrought austenitic stainless per ASME B16.9 in ASTM A403 WP304 — the fitting specification that serves the austenitic bench as A234 serves the chrome-moly grades and A815 the duplexes — welded to the pipe with the line's qualified stainless procedure and ER308-class filler. That butt weld is the joint's only weld, and it belongs entirely to the stub end: the backing flange never enters the procedure. The matching rules are the pattern's usual dimensional ones — lap OD to the flange's shoulder, schedule to the line bore, B16.9 Type A or B lap details to order — plus the austenitic documentary one: dual 304/304L designations stated identically on both certificates where the heats qualify, pairs certified together on one EN 10204 document. On hygienic systems the stub end's lap face is often specified with a finish callout — state it and the lap is machined and polished to suit.
Does an F304 backing flange need PWHT or a weld procedure?
No — though honesty compels a note: on this grade the famous dodge buys less than anywhere else on the bench. Austenitic stainless is the easy end of the welding world — no preheat, no PWHT, no hardenability drama — so a welded 304 flange type carries nothing like the burden a chrome-moly or duplex one does, and the ring's never-welded status saves procedure paperwork rather than furnace time. What the pattern genuinely buys on 304 lines is the rest of its portfolio: the alloy economy (the original story — a carbon steel ring behind a stainless stub end), the rotation that aligns bolt holes on pipework broken and remade constantly, and the sensitization immunity of a ring no weld ever touches. The discipline that exists concentrates on the stub end's single butt weld — qualified procedure, clean purge, ER308-class filler — welded once. The dodge covers the flange, not the joint, here as everywhere.
What sizes and pressure classes do F304 lap joint flanges come in?
½" to 24" NB per ASME B16.5 in Classes 150, 300, 400, 600, 900, 1500 and 2500, with larger diameters machined to B16.47 or drawing — the full class-by-class lap joint dimension charts are on this site. The order book mirrors the grade's habitat: hygienic, water and general process duty concentrates overwhelmingly in Classes 150 and 300 — the austenitic bench's home classes — with the higher classes appearing on cryogenic and gas systems. Dimensionally an F304 lap joint flange is identical to any other grade's — B16.5 governs by class, not by material — so the charts serve every grade on the bench; what changes is the rating table behind the class, where the austenitic group's faster hot derating deserves a check on warm duty. State size, class and the stub-end question together, and our quotation returns price, unit weight and delivery per class.
How much does an F304 lap joint flange weigh?
Exactly what the same-size lap joint flange weighs in any other steel — B16.5 fixes the dimensions by class, and alloy density differences are negligible. Representative Class 150 figures for the flange alone: 1" roughly 0.8 kg, 2" roughly 2 kg, 4" roughly 5.5 kg, 8" roughly 14 kg, climbing steeply with class; the A403 WP304 stub end adds its schedule-dependent mass. The commercial arithmetic is this bench's gentlest: 304 is the least expensive stainless on the site, so the gap between the stainless answer and the economy's carbon steel ring is smaller here than anywhere on the alloy bench — often small enough that the washdown and cryo arguments settle it. Our quotations state unit and consignment weights per line item, flange and stub end separately, and the site's flange weight chart carries the full reference tables.
How are your F304 lap joint flanges manufactured?
As the pattern's standard sequence with austenitic care at the machining and finishing steps. Certified A182 F304 forgings are solution annealed and quenched — furnace records retained — then machined to B16.5's lap joint dimensions: OD, thickness and bolt circle to class, bore and shoulder turned to suit the stub end's lap, and the shoulder radius dressed to bear evenly on the back of the lap; 304's work-hardening makes that machining tougher than the numbers suggest, a manufacturing problem we own so you don't. Chemistry is certified per heat with dual 304/304L designations stated where the heat qualifies. The finish is stainless's own: pickled and passivated, restoring the passive film over every machined surface — never painted, never galvanised. Heat-number marking transfers at the first operation. No welding is performed on the flange at any stage. Where the order includes A403 WP304 stub ends, the pair is dimensionally matched and certified together on one EN 10204 3.1 document (3.2 witnessed on request). Packed sea-worthy with laps and shoulders protected.
What details are needed to get an accurate F304 lap joint flange quotation?
Seven elements plus commercial terms: (1) size and dimensional standard — e.g. 4" NB ASME B16.5; (2) pressure class — 150 to 2500; (3) the grade as your specification writes it — 304, 304L, dual 304/304L (our stock answer) or 304H, each stated exactly on the certificate; (4) the stub end — A403 WP304 matched pair with schedule and B16.9 type, or 'flange only', or the economy answer's carbon steel ring quoted from our A105 page; (5) the service where it helps — chlorides steer the conversation to 316L or the duplex bench, cryogenic duty confirms the stainless ring's advantage; (6) certification — EN 10204 3.1 (our standard) or 3.2 witnessed, pairs certified together on one document; (7) quantity as pairs or pieces, and destination. Quotations normally return within 24 hours with price, unit weights for both parts, and delivery.
Who manufactures ASTM A182 F304 lap joint flanges in India?
Tesco Steel & Engineering is an ISO 9001:2015 certified flange manufacturer based in Mumbai, India, producing ASTM A182 F304 lap joint (lapped joint) flanges per ASME B16.5 from ½" to 24" NB (larger to B16.47 or drawing) in Classes 150-2500 — each machined from certified, solution-annealed S30400 forgings, dual-certified 304/304L where the heat qualifies, pickled and passivated, with the shoulder dressed to bear evenly on the lap, heat-number marked, and certified to EN 10204 3.1/3.2. Matched A403 WP304 stub ends per B16.9 are supplied against the same order, pairs certified together on one document — or the economy answer's carbon steel backing rings from our A105 range, where the specification takes that door. Alongside the complete A182 F304 range — weld neck, slip-on, socket weld, threaded, blind, spectacle blind and long weld neck — the 316L and duplex rungs of the chloride ladder, and the complete lap joint grade bench. Exported to more than 50 countries.