ASTM A182 F53 Lap Joint Flanges — Super Duplex 2507 Backing Flanges & Stub Ends
Tesco Steel & Engineering manufactures ASTM A182 F53 lap joint flanges — the chloride ladder's summit at the lap joint bench: super duplex 2507 (UNS S32750, W.Nr. 1.4410), its escalation over 2205 reading clearly — chromium up three points, molybdenum's ceiling at 5%, and the nitrogen floor tripled — for a pitting number above 40 against hot seawater and aggressive brines, with the strongest stainless certificate on this site: 800 MPa tensile, 550 MPa yield. At this alloy level the match answer dominates: the specifications that justify 2507 almost always put super duplex on both halves of the joint. And the weld dodge is worth the most on the duplex bench here: the ring never welds, so it never enters a phase-balance discipline whose margins are narrower than 2205's — the single butt weld belongs to the A815 S32750 stub end per B16.9. Per ASME B16.5, ½″–24″ NB, Classes 150–2500, solution annealed, pickled & passivated. Every lot with EN 10204 3.1/3.2 MTC. ISO 9001:2015, made in Mumbai, India — exported to 50+ countries.
ASTM A182 F53 Lap Joint Flanges — Specifications at a Glance
What is an ASTM A182 F53 Lap Joint Flange?
The summit's backing flange. An ASTM A182 F53 lap joint flange is the loose backing ring of the two-piece system in super duplex 2507 (UNS S32750) — PREN above 40 for hot seawater and aggressive brines, at 800/550 MPa: the strongest stainless certificate on this site. The point on this pattern: the duties that justify 2507 usually put super duplex on both halves — the ring lives in the same salt air as the line — and the ring never welds, escaping a phase-balance discipline with narrower margins than 2205's; the single butt weld belongs to the stub end. Per ASME B16.5, ½″–24″ NB, Classes 150–2500, solution annealed, pickled & passivated; stub ends A815 S32750 per B16.9. EN 10204 3.1 on every lot.
0.24–0.32% — the floor tripled, at 16× in the PREN formula
Pitting number
PREN above 34
PREN above 40 — the summit
Yield strength
450 MPa
550 MPa — the strongest stainless certificate here
And the price of the summit, stated honestly: elongation's floor drops from 25% to 15%, manganese and silicon are held tighter because intermetallic phases form more readily at this alloy level, and the service band's hot wall moves down — the notes below carry both.
What the Pattern Gives This Grade
The Summit's Strength
800 MPa tensile, 550 MPa yield — compact Class 900–1500 joints on injection and hydraulic duty that an austenitic ring could not carry: the duplex strength argument at full volume.
The Tripled Nitrogen Floor
0.24–0.32% nitrogen — the austenite balancer and the PREN multiplier at 16× — the single cell that most separates 2507's certificate from 2205's.
The Dodge, at Its Narrowest Margins
Super duplex welds under a tighter heat-input window than 2205, and intermetallics punish carelessness fast — and the ring never welds: no procedure, no ferrite count, and no stress relief exists to go wrong.
The Twin Certainty
S32750 here, S32760 on the F55 page — two routes to the same 40-PREN destination; a specification naming either gets exactly that grade and UNS on the certificate, both halves stated identically.
Specification Notes — Getting F53 Lap Joints Right
Three honest notes.The band's walls sharpen at the summit: roughly −50 °C to +250–300 °C — at 25% chromium, 475 °C embrittlement and sigma phase arrive faster than in 2205, and no stress-relieving heat treatment is ever applied. Beyond the summit, change families: water that pits 2507 is not asking for more stainless — it reads the nickel-alloy and titanium pages, where different chemistry takes over. And the pattern's boundaries apply in any grade: heavy external loads, severe vibration and high-moment positions read the weld neck bench — lap joints earn their place where lines dismantle; the hub page states the boundaries fully.
How Our F53 Lap Joint Flanges Are Manufactured
1
Material — certified A182 F53 forgings, solution annealed and quenched with the care 25% chromium demands, furnace records retained; heat-number transfer at the first operation.
2
Machining — B16.5 lap joint dimensions: OD, thickness, bolt circle to class; bore and shoulder turned to suit the stub end's lap.
3
Shoulder dressing — the radius dressed to bear evenly on the back of the lap — spreading bolt load instead of concentrating it.
4
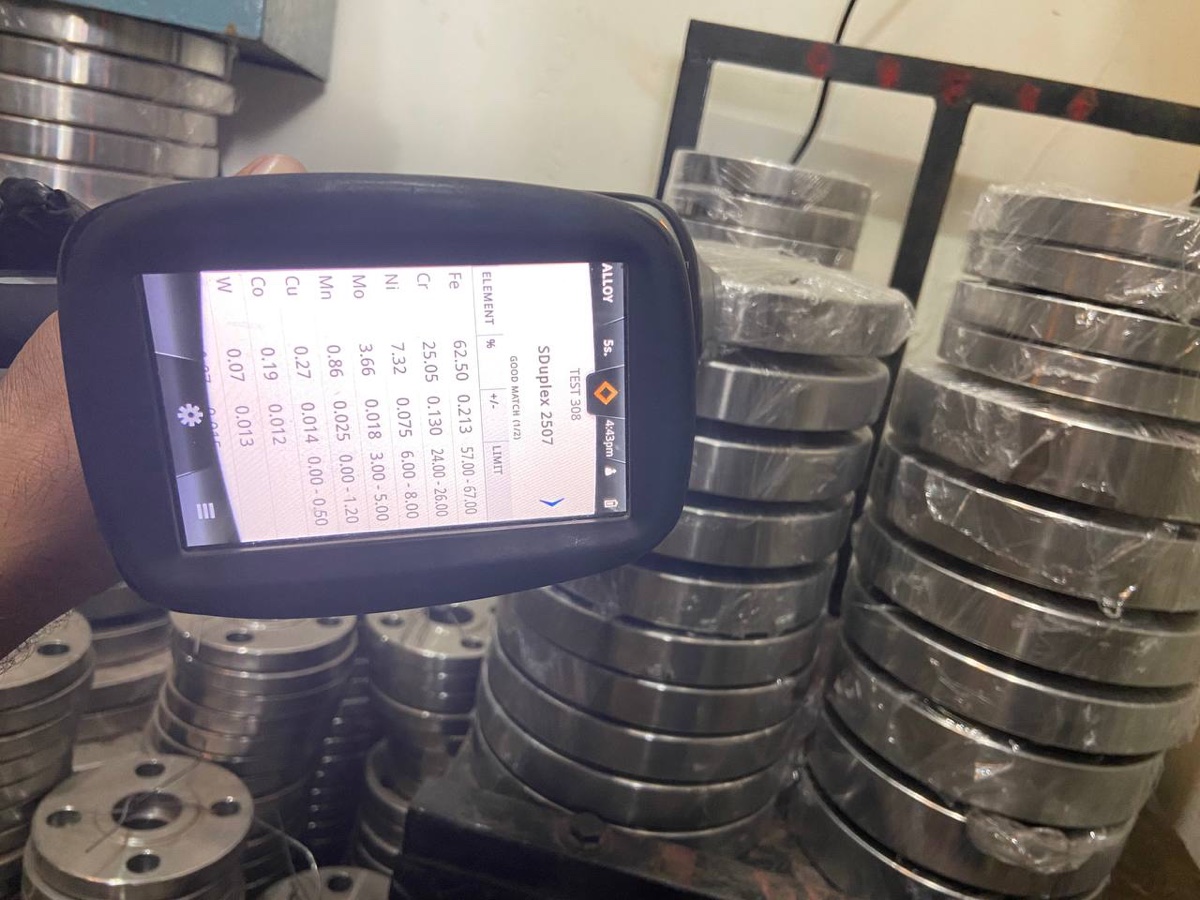
Testing — PMI reads the Cr-Mo-N signature that separates 2507 from 2205 in seconds; chemistry and mechanicals certified per heat.
5
Pickling & passivation — the family's own finish, restoring the passive film — never painted, never galvanised; and no welding, ever — the ring keeps its solution-annealed structure for life.
6
Pairing & certification — matched to A815 S32750 stub ends where ordered; one EN 10204 3.1 document per pair (3.2 witnessed on request); packed sea-worthy with laps and shoulders protected.
Where F53 Lap Joint Flanges Are Used
Where the summit's water and the pattern meet: offshore seawater lift and injection systems, firewater ring mains and deluge headers whose spools dismantle for inspection, desalination high-pressure brine trains, and the hot, saline process duty where 2205 pits — specifically the positions that earn a lap joint: dismantling seawater headers, rotating spools on erosive brine duty, and compact Class 900–1500 joints where the summit's yield carries the bolting. Production and supply below:
F53 Super Duplex — Laser-Marked S32750 TraceabilityThe Two-Piece System — Flange, Stub End, Butt Weld, PipePMI Verification — The Cr-Mo-N Signature, Proven
F53 Lap Joint Flange Dimensions
Flange dimensions are class-governed per ASME B16.5 — identical in every grade; stub ends per B16.9. Full class-by-class charts:
Example: “Lap Joint Flange, 8″ NB, ASME B16.5 Class 300, ASTM A182 F53 (UNS S32750), with A815 S32750 stub ends Sch 40S (B16.9 Type A, supplied together), pairs on one MTC, EN 10204 3.1 — 12 sets.” Quotations normally within 24 hours with price, unit weights (both parts) and delivery.
F53 Lap Joint Flanges — Frequently Asked Questions
What is an ASTM A182 F53 lap joint flange?
An ASTM A182 F53 lap joint flange is the loose backing flange of the two-piece lap joint system, forged in super duplex 2507 (UNS S32750, W.Nr. 1.4410) — the chloride ladder's summit grade, whose chromium, molybdenum and tripled nitrogen floor put its pitting resistance number above 40 for hot seawater and aggressive brines, and whose 550 MPa yield is the strongest stainless certificate on this site. Like every lap joint flange it slides over the pipe, sits free behind the stub end's flared lap, and carries the entire bolt load without touching the line fluid — and because it never welds, it never enters super duplex's phase-balance welding discipline; the joint's single butt weld belongs to the stub end. Manufactured per ASME B16.5 in ½" to 24" NB, Classes 150 to 2500, solution annealed, pickled and passivated, with EN 10204 3.1/3.2 certification on every lot.
How does the two-piece lap joint system work?
By splitting sealing from bolting. The stub end butt-welds to the pipe: its flared lap provides the gasket face and does all the fluid contact. The backing flange never welds and never wets: it slides on before the stub end is welded — the classic site lesson — spins freely until the bolts enter, and transmits bolt load through its radiused shoulder onto the back of the lap. On the duplex pages of this bench the pattern's argument runs on chemistry — chlorides only touch what wets — and at the summit the argument sharpens: the duties that justify 2507 are hot, saline and unforgiving, usually offshore, and the specifications that govern them almost always put super duplex on both halves of the joint, as the next FAQ explains. The full pattern story — stub end types, the alloy economy, the honest boundaries — is on the lap joint hub page.
Does the backing flange behind a super duplex line need to be super duplex?
Almost always yes — and the reasons are the F51 page's match answer, turned up. In principle the pattern's economy applies here too: the ring never wets, so a cheaper ring could back a 2507 stub end. In practice the duties that justify super duplex — hot seawater lifts, firewater deluge, aggressive brine trains, splash-zone and topside process systems — put the ring itself in salt-laden air and deluge water for decades, where coated carbon steel is a maintenance liability and galvanised surfaces are unwelcome near stainless welding. Offshore piping classes in the NORSOK tradition write matched super duplex through the joint, and audit certificates accordingly. So this page's normal order is F53 backing an A815 S32750 stub end, pairs on one document; where an inland or sheltered specification genuinely takes the economy door, our A105 page quotes that ring — say so on the enquiry and both options price in a day.
What is the chemical composition of ASTM A182 F53 (UNS S32750)?
Carbon ≤0.030%, manganese ≤1.20%, silicon ≤0.80%, chromium 24.0-26.0%, nickel 6.0-8.0%, molybdenum 3.0-5.0%, nitrogen 0.24-0.32%, copper ≤0.50%, phosphorus ≤0.035%, sulphur ≤0.020%. Against 2205 the escalation reads clearly: chromium up three points, molybdenum's ceiling up to 5%, and the nitrogen floor tripled — nitrogen being both the austenite balancer and the PREN multiplier at 16×. Manganese and silicon are held tighter than 2205's because intermetallic phases form more readily at this alloy level. Note copper is a residual cap here, not an addition — the deliberately copper-and-tungsten-alloyed sibling is F55 (S32760). Chemistry is verified per heat and travels on the EN 10204 3.1 MTC.
What are the mechanical properties of F53 lap joint flanges?
In the solution-annealed condition A182 requires tensile strength 800 MPa (116 ksi) minimum, yield strength 550 MPa (80 ksi) minimum and elongation 15% minimum — the strongest stainless certificate on this site, above duplex 2205's 450 MPa yield and far above any austenitic grade. For the backing-flange duty that strength is the summit's version of the duplex argument: the ring's whole job is bolting and bending, and at Class 900-1500 offshore injection and hydraulic duty the stiffer, stronger ring carries compact high-class joints that an austenitic ring could not. The honest counterpart is the 15% elongation floor — lower than 2205's 25%, the usual price of strength. Where a design needs more still, the strength ladder on this site continues into the nickel and titanium worlds; for chloride duty, F53 is already at the practical summit of stainless. Supplied with the solution-anneal records retained.
F53 or F55 — what is the difference between the super duplex twins?
Two routes to the same 40-PREN destination. F53 (S32750, 2507) is the 'lean-alloyed' route: chromium, molybdenum and nitrogen alone. F55 (S32760, the Zeron 100 type) adds deliberate copper and tungsten — 0.5-1.0% of each — claiming extra margin in acidic and erosive seawater conditions, and it carries its own dedicated following in UK-influenced offshore specifications. In practice their performance envelopes overlap almost completely, both are solution-annealed, both weld under the same discipline, and the choice is nearly always made by the project specification rather than by metallurgy: North Sea heritage documents tend to name S32760, others 2507. We forge both — a specification naming either gets exactly that grade and UNS number on the certificate, and F55 has its own lap joint page on this site. On a matched-pair order the twin question applies to both halves: flange and stub end carry the same UNS, stated identically.
What are the temperature limits of super duplex 2507?
The duplex family band, slightly sharpened: roughly -50°C to +250-300°C. Cold: the ferrite half's ductile-brittle transition draws the same ~-46 to -50°C line as 2205, below which austenitics or nickel steels take over. Hot: at 25% chromium the embrittlement chemistry is more eager than 2205's — 475°C embrittlement and sigma phase both arrive faster — so design codes cap sustained super duplex service around 250-300°C and prohibit any stress-relieving heat treatment. Inside the band the grade is untouchable on its own ground: hot chloride duty that pits everything below it. The lap joint ring lives comfortably there — chloride service sits well inside the walls — and as everywhere on this bench, the contrast with the chrome-moly pages is the point: the super duplex ring's constraint is chemistry and climate, never heat. Specifications that push either wall get an honest grade change on our quotation.
What stub ends pair with F53 lap joint flanges?
The matching stub end is wrought super duplex per ASME B16.9 in ASTM A815 UNS S32750 — the ferritic/austenitic fitting specification serving the duplex family — welded to the pipe with the line's qualified super duplex procedure: ER2594-class filler, a controlled heat-input window tighter than 2205's, and phase balance verified in the weld zone, because at this alloy level intermetallics punish carelessness quickly. That butt weld is the joint's only weld, and it belongs entirely to the stub end: the backing flange never enters the procedure. The matching rules are the pattern's usual dimensional ones — lap OD to the flange's shoulder, schedule to the line bore — plus the summit's documentary one: the same UNS on both certificates, stated identically, pairs certified together on one EN 10204 document. Where an order needs B16.9 Type A or Type B lap details, state it and the pair is machined to suit.
Does an F53 backing flange need PWHT or a weld procedure?
No — and at the summit the dodge is worth more than anywhere else on the duplex bench. Welding super duplex is the duplex discipline with narrower margins: the heat-input window is tighter, intermetallic phases form faster at 25% chromium, ferrite balance is checked more jealously, and there is still no thermal escape hatch — stress-relieving heat treatment is never applied, because every reheat courts the embrittlement the grade must avoid. The lap joint backing ring inherits none of this, because it is never welded to anything: no procedure, no ferrite count, no heat-input anxiety — the solution-annealed structure it left the furnace with is the structure it keeps for life. The discipline concentrates on the joint's single butt weld — stub end to pipe, welded once under the line's qualified super duplex procedure. The dodge covers the flange, not the joint — the stub end's weld takes the full discipline, always.
Where does F53 sit on the chloride ladder?
At the summit — the practical top of stainless for chloride duty. The ladder climbs by pitting number: 316L and the austenitic bench carry brackish and mildly saline duty economically; F51 duplex 2205 takes over above 34 PREN for seawater-adjacent systems and brines, adding doubled yield; and the super duplex pair — F53 (S32750) and F55 (S32760) — reach PREN above 40 for hot seawater, aggressive and acidic brines, and the duties where 2205 pits, at 550 MPa yield. Beyond the summit the ladder leaves stainless altogether: duties that attack even super duplex read the nickel-alloy and titanium pages of this site, where different chemistry rather than more of the same takes over. The honest advice runs both ways, as everywhere here: water that 2205 handles gains nothing from the summit's premium, and water that pits 2507 names its chemistry and changes families. State the water and the rung picks itself.
What sizes and pressure classes do F53 lap joint flanges come in?
½" to 24" NB per ASME B16.5 in Classes 150, 300, 400, 600, 900, 1500 and 2500, with larger diameters machined to B16.47 or drawing — the full class-by-class lap joint dimension charts are on this site. The order book mirrors the grade's habitat: seawater and firewater systems concentrate in Classes 150 and 300 at mid and large bore, with injection, hydraulic and process duty running Classes 600 to 1500 where the summit's 550 MPa yield earns compact joints. Dimensionally an F53 lap joint flange is identical to any other grade's — B16.5 governs by class, not by material — so the charts serve every grade on the bench; what changes is the material behind the dimensions and, on offshore projects, the certification package behind that. State size, class and the stub-end question together, and our quotation returns price, unit weight and delivery per class.
How much does an F53 lap joint flange weigh?
Exactly what the same-size lap joint flange weighs in any other steel — B16.5 fixes the dimensions by class, and alloy density differences are negligible. Representative Class 150 figures for the flange alone: 1" roughly 0.8 kg, 2" roughly 2 kg, 4" roughly 5.5 kg, 8" roughly 14 kg, climbing steeply with class; the A815 stub end adds its schedule-dependent mass. The commercial difference sits in the metallurgy and the paperwork: F53 carries the super duplex alloy surcharge — the summit's price — plus solution annealing and per-lot testing, yet still lands well below the nickel alloys it replaces on hot chloride duty, which is the grade's whole commercial argument. Our quotations state unit and consignment weights per line item, flange and stub end separately, and the site's flange weight chart carries the full reference tables.
How are your F53 lap joint flanges manufactured?
As the pattern's standard sequence with summit discipline at the heat-treatment and finishing steps. Certified A182 F53 forgings are solution annealed and quenched — the treatment that sets the fifty-fifty structure, run with the care 25% chromium demands, furnace records retained — then machined to B16.5's lap joint dimensions: OD, thickness and bolt circle to class, bore and shoulder turned to suit the stub end's lap, and the shoulder radius dressed to bear evenly on the back of the lap. Chemistry is certified per heat with PMI reading the Cr-Mo-N signature that separates 2507 from 2205 in seconds. The finish is the family's own: pickled and passivated, restoring the passive film over every machined surface — never painted, never galvanised. Heat-number marking transfers at the first operation. No welding is performed on the flange at any stage — the ring keeps its solution-annealed structure for life. Where the order includes A815 S32750 stub ends, the pair is dimensionally matched and certified together on one EN 10204 3.1 document (3.2 witnessed on request). Packed sea-worthy with laps and shoulders protected.
What details are needed to get an accurate F53 lap joint flange quotation?
Seven elements plus commercial terms: (1) size and dimensional standard — e.g. 6" NB ASME B16.5; (2) pressure class — 150 to 2500; (3) the designation as your specification writes it — F53, S32750 or 2507; where the document names S32760 or Zeron-type material it is asking for F55, the twin with its own page and its own certificate; (4) the stub end — A815 S32750 matched pair with schedule and B16.9 type, or 'flange only'; (5) the water where it helps — chloride level and temperature confirm the summit, and chemistry beyond it changes families to the nickel alloys; (6) certification — EN 10204 3.1 (our standard) or 3.2 witnessed, pairs certified together on one document; (7) quantity as pairs or pieces, and destination. Quotations normally return within 24 hours with price, unit weights for both parts, and delivery.
Who manufactures ASTM A182 F53 lap joint flanges in India?
Tesco Steel & Engineering is an ISO 9001:2015 certified flange manufacturer based in Mumbai, India, producing ASTM A182 F53 super duplex 2507 lap joint (lapped joint) flanges per ASME B16.5 from ½" to 24" NB (larger to B16.47 or drawing) in Classes 150-2500 — each machined from certified, solution-annealed S32750 forgings, PMI-checked on the Cr-Mo-N signature, pickled and passivated, with the shoulder dressed to bear evenly on the lap, heat-number marked, and certified to EN 10204 3.1/3.2. Matched A815 S32750 stub ends per B16.9 are supplied against the same order, pairs certified together on one document. Alongside the complete A182 F53 range — weld neck, slip-on, socket weld, threaded, blind, spectacle blind and long weld neck — the twin F55, the duplex rung F51, and the complete lap joint grade bench. Exported to more than 50 countries.