

'SHAPING INDUSTRIES WITH THE FINEST STEEL'
'SHAPING INDUSTRIES WITH THE FINEST STEEL'
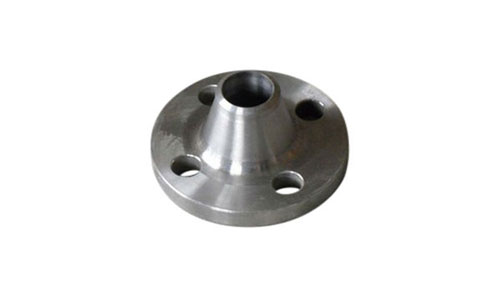
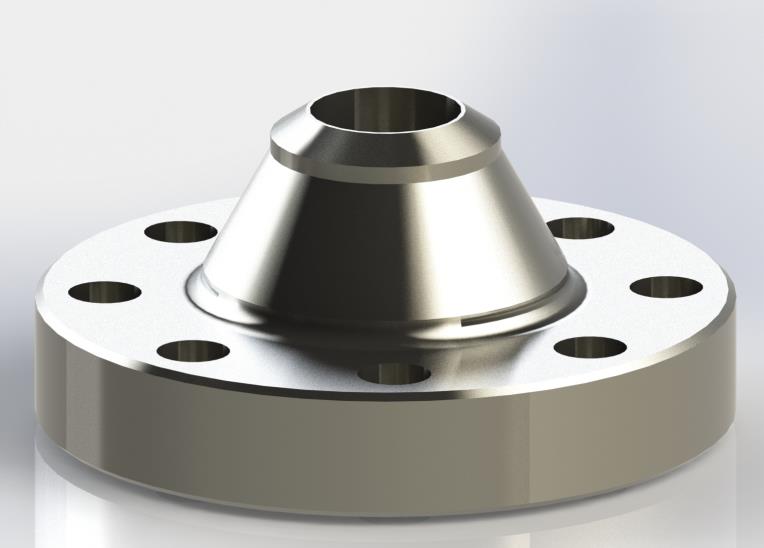
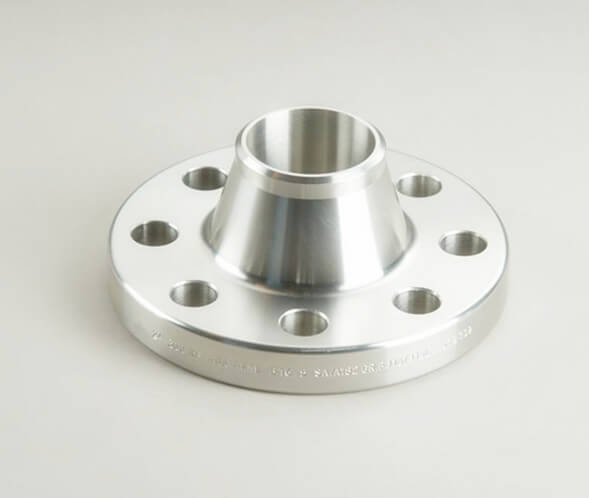
Tesco Steel & Engineering manufactures ASME B16.5 Class 300 weld neck flanges — the step-up class where pressure or temperature outgrows Class 150 — in NPS 1/2 to 24 (DN 15–600), raised face or ring type joint, with the bore matched to your pipe schedule. This page is the complete reference for the class: the full dimension chart in mm with approximate weights in kg and lbs, the stud & bolt chart, pressure-rating guidance and every material grade we produce — from A105 and A350 LF2 to SS 316, duplex and Inconel. ISO 9001:2015 certified, made in Mumbai, India — exported worldwide.
If Class 150 is where most of the world’s flanges live, Class 300 is where the working lines live: steam headers, condensate returns, hot oil circuits, boiler feed, refinery process piping — services with genuine pressure, and almost always genuine temperature with it. That combination is exactly what the class is built for, because B16.5 ratings fall as metal heats up, and Class 300 keeps a comfortable margin at temperatures where Class 150 has already surrendered most of its rating.
Within the class, the weld neck is the default type rather than the premium option: at these pressures the tapered hub and full-penetration butt weld — a joint as strong as the pipe itself, open to radiography — are what most line classes specify, with slip-on and socket-weld versions reserved for milder duty. The tables below are the working data: flange dimensions in millimetres against the lettered diagram, published weights in kg with our lbs conversion, and the bolt chart with stud and machine-bolt lengths, PCD and hole sizes. All values follow ASME B16.5; bores are finished to the pipe schedule you specify.
“Class 300” (also written #300 or 300 lb) is a pressure–temperature rating class, not a fixed working pressure — and certainly not 300 psi. ASME B16.5 tabulates, for every material group, the maximum allowable working pressure at each temperature. Two useful anchors for Group 1.1 carbon steel (A105):
All dimensions in mm. Letters follow the ASME B16.5 figure: O = outer diameter, C = flange thickness, X = hub diameter at base, A = hub diameter at the weld bevel, V = length through hub, R = raised face diameter, H = raised face height, B = bolt circle (PCD). C and V are the full B16.5 tabulated values, measured including the 2 mm raised face; the bore and the 1.6 mm weld-end land carry no letter on the figure. The two right-hand columns give the weight per flange in kg (published, carbon steel, standard bore) and our lbs conversion. Prefer it on paper? Download the full Class 300 weld neck dimensions datasheet (PDF) — the same table with the drawing, bolting and weights, ready for the workshop.
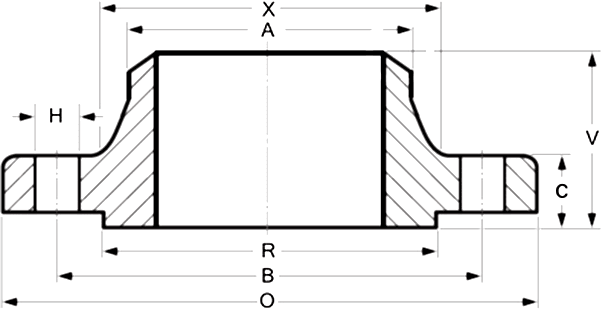
Weld Neck Flange Dimension Reference — ANSI / ASME B16.5
| Size in Inch | Size in mm | Outer Diameter | Flange Thickness | Hub OD | Weld Neck OD | Length Through Hub | Bore | RF Diameter | RF Height | PCD | Weld Face | Approx Weight (kg) | Approx Weight (lbs) |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| O | C | X | A | V | — | R | H | B | — | ||||
| 1/2 | 15 | 95 | 14.3 | 38 | 21.3 | 52 | According to Schedule | 34.9 | 2 | 66.7 | 1.6 | 0.9 | 2.0 |
| 3/4 | 20 | 115 | 15.9 | 48 | 26.7 | 57 | 42.9 | 2 | 82.6 | 1.6 | 1.4 | 3.1 | |
| 1 | 25 | 125 | 17.5 | 54 | 33.4 | 62 | 50.8 | 2 | 88.9 | 1.6 | 1.8 | 4.0 | |
| 1 1/4 | 32 | 135 | 19.1 | 64 | 42.2 | 65 | 63.5 | 2 | 98.4 | 1.6 | 2.3 | 5.1 | |
| 1 1/2 | 40 | 155 | 20.7 | 70 | 48.3 | 68 | 73 | 2 | 114.3 | 1.6 | 3.2 | 7.1 | |
| 2 | 50 | 165 | 22.4 | 84 | 60.3 | 70 | 92.1 | 2 | 127 | 1.6 | 4.1 | 9.0 | |
| 2 1/2 | 65 | 190 | 25.4 | 100 | 73 | 73 | 104.8 | 2 | 149.2 | 1.6 | 5.4 | 11.9 | |
| 3 | 80 | 210 | 28.6 | 117 | 88.9 | 79 | 127 | 2 | 168.3 | 1.6 | 6.8 | 15.0 | |
| 3 1/2 | 90 | 230 | 30.2 | 133 | 101.6 | 81 | 139.7 | 2 | 184.2 | 1.6 | 8.2 | 18.1 | |
| 4 | 100 | 255 | 31.8 | 146 | 114.3 | 86 | 157.2 | 2 | 200 | 1.6 | 11.3 | 24.9 | |
| 5 | 125 | 280 | 35 | 178 | 141.3 | 98 | 185.7 | 2 | 235 | 1.6 | 14.5 | 32.0 | |
| 6 | 150 | 320 | 36.6 | 206 | 168.3 | 98 | 215.9 | 2 | 269.9 | 1.6 | 19.1 | 42.1 | |
| 8 | 200 | 380 | 41.3 | 260 | 219.1 | 111 | 269.9 | 2 | 330.2 | 1.6 | 30.4 | 67 | |
| 10 | 250 | 445 | 47.7 | 321 | 273 | 117 | 323.8 | 2 | 387.4 | 1.6 | 41.3 | 91 | |
| 12 | 300 | 520 | 50.8 | 375 | 323.8 | 130 | 381 | 2 | 450.8 | 1.6 | 63.5 | 140 | |
| 14 | 350 | 585 | 54 | 425 | 355.6 | 143 | 412.8 | 2 | 514.4 | 1.6 | 81.6 | 180 | |
| 16 | 400 | 650 | 57.2 | 483 | 406.4 | 146 | 469.9 | 2 | 571.5 | 1.6 | 113 | 249 | |
| 18 | 450 | 710 | 60.4 | 533 | 457.2 | 159 | 533.4 | 2 | 628.6 | 1.6 | 145 | 320 | |
| 20 | 500 | 775 | 63.5 | 587 | 508 | 162 | 584.2 | 2 | 685.8 | 1.6 | 181 | 399 | |
| 22 | 550 | 840 | 66.7 | 641 | 558.8 | 165 | 641.4 | 2 | 743 | 1.6 | 211 | 465 | |
| 24 | 600 | 915 | 69.9 | 702 | 610 | 168 | 692.2 | 2 | 812.8 | 1.6 | 263 | 580 |
Bolt quantities and UNC sizes with both machine bolt and raised-face stud lengths (mm), bolt hole sizes and metric equivalents per flange size. At Class 300, stud bolts with two heavy hex nuts are the standard practice — machine bolts survive only on mild utility duty. Note the 8-bolt pattern arriving already at 2″, where Class 150 still uses 4. See also our fastener weight & count chart.
| Size in Inch | Size in mm | No of Bolts | Bolt Size UNC | Machine Bolt Length | RF Stud Length | Hole Size | ISO Stud Size |
|---|---|---|---|---|---|---|---|
| 1/2 | 15 | 4 | 1/2 | 55 | 65 | 5/8 | M14 |
| 3/4 | 20 | 4 | 5/8 | 65 | 75 | 3/4 | M16 |
| 1 | 25 | 4 | 5/8 | 65 | 75 | 3/4 | M16 |
| 1 1/4 | 32 | 4 | 5/8 | 70 | 85 | 3/4 | M16 |
| 1 1/2 | 40 | 4 | 3/4 | 75 | 90 | 7/8 | M20 |
| 2 | 50 | 8 | 5/8 | 75 | 90 | 3/4 | M16 |
| 2 1/2 | 65 | 8 | 3/4 | 85 | 100 | 7/8 | M20 |
| 3 | 80 | 8 | 3/4 | 90 | 110 | 7/8 | M20 |
| 3 1/2 | 90 | 8 | 3/4 | 95 | 110 | 7/8 | M20 |
| 4 | 100 | 8 | 3/4 | 95 | 115 | 7/8 | M20 |
| 5 | 125 | 8 | 3/4 | 110 | 120 | 7/8 | M20 |
| 6 | 150 | 12 | 3/4 | 110 | 120 | 7/8 | M20 |
| 8 | 200 | 12 | 7/8 | 120 | 140 | 1 | M24 |
| 10 | 250 | 16 | 1 | 140 | 160 | 1 1/8 | M27 |
| 12 | 300 | 16 | 1 1/8 | 145 | 170 | 1 1/4 | M30 |
| 14 | 350 | 20 | 1 1/8 | 160 | 180 | 1 1/4 | M30 |
| 16 | 400 | 20 | 1 1/4 | 165 | 190 | 1 3/8 | M33 |
| 18 | 450 | 24 | 1 1/4 | 170 | 195 | 1 3/8 | M33 |
| 20 | 500 | 24 | 1 1/4 | 185 | 205 | 1 3/8 | M33 |
| 22 | 550 | 24 | 1 1/2 | 190 | 210 | 1 5/8 | M39 |
| 24 | 600 | 24 | 1 1/2 | 205 | 230 | 1 5/8 | M39 |
Class 300 weld neck flanges are produced in every material family from our range — each supplied with EN 10204 3.1 mill certificates, heat-number traceability and PMI on request:
| Material Family | Typical Flange Grades | Best suited to |
|---|---|---|
| Carbon Steel | ASTM A105, A694 F42–F65 | General & high-pressure hydrocarbon service |
| LTCS | ASTM A350 LF2 / LF3 | Low-temperature service, impact tested |
| Stainless Steel | A182 F304/L, F316/L, F310, F321, F347, F410 | Corrosive process & hygienic service |
| 254 SMO | A182 F44 (UNS S31254) | Seawater & high-chloride service |
| 904L | A182 F904L (UNS N08904) | Sulphuric & phosphoric acid service |
| Duplex / Super Duplex | A182 F51 (2205), F53/F55 (2507) | High strength + chloride resistance, offshore |
| Alloy Steel | A182 F1, F5, F9, F11, F22, F91 | High-temperature steam & refinery lines — classic Class 300 territory |
| Monel | 400 / K500 (B564 N04400) | Seawater, HF acid, marine |
| Inconel | 600 / 601 / 625 / 825 | High temperature, sour & oxidising media |
| Hastelloy | C276 / C22 / B2 | Severely corrosive chemical service |
| Titanium | Gr. 2 / Gr. 5 (B381) | Chlorides, seawater; ≈42% lighter |
| Copper Nickel | 90/10 (C70600), 70/30 (C71500) | Marine & seawater cooling systems |
| Bimetal / Clad | CS base + SS/alloy overlay | Corrosion resistance at carbon-steel cost |
Prices are competitive and standard sizes are held in ready stock — use the Ask for Quote button or the inquiry form for today’s price list and stock position.
| Pressure Class | Dimension Chart | Approx. A105 Rating @ 38 °C |
|---|---|---|
| Class 150 | Class #150 Weld Neck Flange | ≈285 psig |
| Class 300 | Class #300 Weld Neck Flange (this page) | ≈740 psig |
| Class 400 | Class #400 Weld Neck Flange | ≈990 psig |
| Class 600 | Class #600 Weld Neck Flange | ≈1480 psig |
| Class 900 | Class #900 Weld Neck Flange | ≈2220 psig |
| Class 1500 | Class #1500 Weld Neck Flange | ≈3705 psig |
| Class 2500 | Class #2500 Weld Neck Flange | ≈6170 psig |
Related references: Weld Neck Flanges overview · Long Weld Neck Flanges · All Flange Dimension Charts · Flange Weight Chart.
The tapered hub and full-penetration butt weld give the joint the strength and fatigue life of the pipe itself — at Class 300 pressures and temperatures, that is not a luxury but the specification.
Class 150 loses its rating quickly as metal heats; Class 300 holds a working margin deep into steam territory — the whole reason the class exists, and the reason hot lines jump straight to it.
The schedule-matched bore removes turbulence and erosion at the joint — no crevice, no flow step, easy radiography of the butt weld on lines where examination is mandatory.
Steam headers and condensate systems, boiler feed and blowdown, hot oil and thermic fluid circuits, refinery and petrochemical process lines, compressed gases, offshore service — wherever pressure and temperature arrive together.
What are the dimensions of a Class 300 weld neck flange?
They are tabulated in ASME B16.5 and reproduced in full in the chart above: for each size from NPS 1/2 to 24, the outer diameter, flange thickness, hub and weld-neck diameters, length through hub, raised face diameter and height (2 mm at this class), bolt circle and weld face — all in millimetres — plus the published weight. A 4 in Class 300 weld neck flange, for example, is 255 mm OD, 31.8 mm thick, on a 200 mm PCD, at about 11.3 kg.
What pressure can a Class 300 flange handle?
The rating depends on material and temperature. For Group 1.1 materials such as A105 carbon steel, ASME B16.5 allows roughly 740 psig (about 51 bar) at 38 °C — some two and a half times Class 150 — and the class holds its rating far better as temperature rises, still offering roughly 550 psig around 300 °C where Class 150 has fallen to about 140. Stainless and alloy grades have their own tables. Always confirm the rating at your design temperature.
What does the "Class 300" designation actually mean?
Class 300 (also written #300 or 300 lb) is a pressure-temperature rating class, not a working pressure of 300 psi. Each class maps to a table in ASME B16.5 giving the maximum allowable working pressure at each temperature for each material group — a Class 300 A105 flange is good for roughly 740 psig cold, comfortably more than the number in its name, and less when hot.
Why do the thickness values here differ from some other Class 300 charts?
Because ASME B16.5 tabulates minimum flange thickness including the 2 mm raised face for Class 150 and 300, and that is how our chart lists it — a 2 in Class 300 flange reads 22.4 mm. Many trade charts print the body thickness with the face deducted (20.7 mm for the same flange) and show the face height in a separate column, which makes two correct charts look 1.6-2 mm apart. Check which convention a chart uses before comparing; ours follows the standard.
How much does a Class 300 weld neck flange weigh?
From the weight columns in our chart: a 2 inch Class 300 weld neck flange weighs about 4.1 kg (9 lbs), a 6 inch about 19 kg (42 lbs), a 12 inch about 64 kg (140 lbs) and a 24 inch about 263 kg (580 lbs) — roughly 50 to 100 percent heavier than Class 150, size for size. These are published carbon-steel weights with a standard bore; the exact weight varies with the bore schedule and material density.
What is the raised face height on a Class 300 flange?
Class 150 and 300 share the light raised face — 2 mm (nominally 1/16 inch), shown in the RF Height column of our chart — whereas Class 400 and above step up to the 6.35 mm (1/4 inch) face. So a take-off moving from 150 to 300 keeps its facing assumptions, but one moving from 300 to 400 or 600 does not — the taller face needs longer studs, and it is a classic estimating miss.
Are Class 150 and Class 300 flanges interchangeable on the same bolt pattern?
No. For every size the Class 300 flange carries a larger outer diameter, a larger bolt circle and usually more or bigger bolts than its Class 150 counterpart — a 4 in flange, for instance, is 230 mm OD on a 190.5 mm PCD at Class 150 but 255 mm OD on a 200 mm PCD at Class 300. A Class 300 flange will never bolt to a Class 150 flange of the same size. When a line changes class at a spec break, the joint needs matching flanges on both sides.
What sizes does ASME B16.5 cover?
ASME B16.5 covers pipe flanges from NPS 1/2 to NPS 24 (DN 15 to DN 600) in classes 150, 300, 400, 600, 900, 1500 and 2500. Flanges larger than 24 inches are covered by ASME B16.47 (Series A and B). Our Class 300 weld neck chart on this page lists twenty-one sizes with dimensions in millimetres, NPS 22 included.
What bore should I specify for a weld neck flange?
The bore of a weld neck flange is machined to match the inside diameter of the pipe it will be welded to, so state the pipe schedule with your order. At Class 300 pressures the mating pipe is commonly Sch 40 or Sch 80 — and the match matters more here than at Class 150, because a bore step at the butt weld concentrates turbulence and erosion exactly where the joint works hardest. That is why the Bore column in our chart reads "as per pipe schedule".
What materials and grades are available for Class 300 weld neck flanges?
We manufacture Class 300 weld neck flanges in carbon steel A105, low-temperature A350 LF2/LF3, stainless steel A182 F304/L, F316/L, F310, F321, F347 and F410, 254 SMO (F44), 904L, duplex 2205 (F51), super duplex 2507 (F53/F55), alloy steel F1/F5/F9/F11/F22/F91, Monel 400/K500, Inconel 600/625/825, Hastelloy C276/C22, titanium, copper nickel 90/10 and 70/30, and bimetal/clad — each with EN 10204 3.1 mill certificates.
Does a Class 300 flange use machine bolts or stud bolts?
Stud bolts with two heavy hex nuts are the standard practice at Class 300, and that is what the RF Stud Length column is for; machine bolts remain acceptable on mild utility duty, so our chart gives both lengths. A 2 inch flange takes 8 bolts of 5/8 inch UNC — note the jump to an 8-bolt pattern already at 2 inches, where Class 150 still uses 4 — a 12 inch takes 16 of 1-1/8 inch, and a 24 inch takes 24 of 1-1/2 inch.
Which gasket is used with Class 300 raised face flanges?
Spiral wound gaskets to ASME B16.20 with an outer centring ring are the default at Class 300 bolt loads, graphite-filled for steam and hydrocarbons and PTFE-filled for chemical duty; quality sheet gaskets remain acceptable on milder services. RTJ facings with oval or octagonal ring gaskets are a routine request at this class for hydrocarbon service — state RF or RTJ with the enquiry.
Why choose a weld neck flange over a slip-on flange at Class 300?
At Class 300 pressures and the temperatures that usually come with them, the weld neck's tapered hub and full-penetration butt weld give the joint the strength and fatigue life of the pipe itself, with a smooth bore, no crevice and a weld that radiography can examine. Slip-on flanges are still permitted at this class, but the case for them weakens as pressure and cycling rise — on steam, hot oil and hydrocarbon lines the weld neck is the standard choice.
What is the difference between Class 300 and Class 150 flanges?
For A105 at 38 °C the allowable working pressures are roughly 740 and 285 psig respectively, and the gap widens dramatically with temperature — around 300 °C a Class 300 flange still carries roughly 550 psig where Class 150 has fallen to about 140. Dimensionally the Class 300 flange is thicker, wider and heavier on a larger bolt circle, on the same light 2 mm raised face. When a service sits near the top of the Class 150 envelope, or sees real temperature, Class 300 is the standard step.
How are your Class 300 flanges tested and certified?
Every batch is dimensionally inspected against ASME B16.5, marked per MSS SP-25 and supplied with EN 10204 3.1 mill test certificates traceable by heat number. We offer PMI, ultrasonic and magnetic particle examination, impact testing for low-temperature grades, NACE MR0175 compliance for sour service, and third-party inspection by LR, BV, DNV, SGS, TÜV or IBR on request.
Do you make the other Class 300 flange types too?
Yes — slip-on, blind, socket weld, lapped joint, long weld neck and spectacle blind dimension charts for Class 300 are all on this site (linked in the sidebar), alongside the weld neck charts for Class 150 and for classes 400 through 2500. Special bores, facings and flanges to customer drawings are quoted case-by-case.
Which industries use Class 300 weld neck flanges?
Class 300 is the workhorse of lines with real pressure or temperature: steam and condensate systems in power plants, refinery and petrochemical process piping, hot oil and thermic fluid circuits, boiler feed and blowdown, compressed gas systems, and offshore service — the territory where Class 150's fast derating rules it out but the heavy classes would be overkill.
Are these the same dimensions as ANSI 300?
Yes — "ANSI 300", "ANSI B16.5" and "300 lb" all refer to what is today the ASME B16.5 Class 300 table; the standard transferred from ANSI to ASME custodianship decades ago but the old name persists on drawings and enquiries. The dimensions on this page are the current ASME B16.5 values.