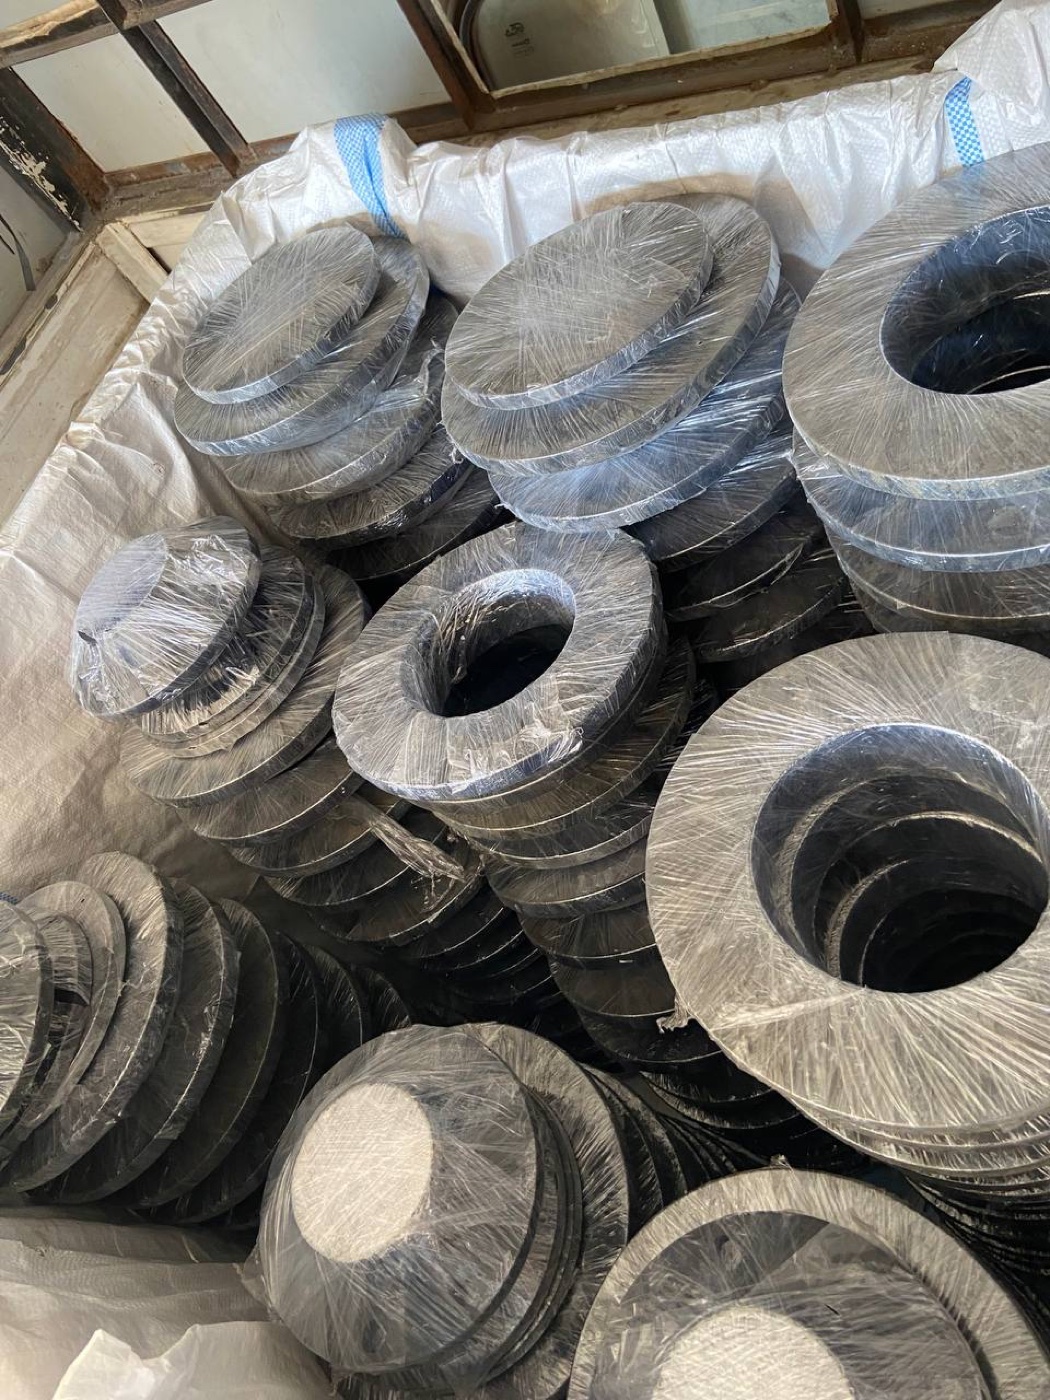
Tesco Steel & Engineering manufactures ASTM A182 F22 lap joint flanges — the chrome-moly staircase's workhorse (UNS K21590, W.Nr. 1.7380) at the lap joint bench: 2¼% chromium and a full 1% molybdenum buying creep-rupture ratings at the hot end of the steam band and the hydrogen-service standing that makes it hydroprocessing's default — the most-stocked, most-specified rung of the family. The pattern's virtues apply in full: the backing ring never welds and never wets — no preheat, no PWHT on the flange; the joint's single butt weld belongs to the matched A234 WP22 stub end per B16.9. The lap joint bench's metal-temperature argument holds at the workhorse rung — the ring runs at line metal temperature, so it cannot be A105 — and the class trap is named plainly: Class 3 is the flange default, and no F22 Class 2 exists in A182. Per ASME B16.5, ½″–24″ NB, Classes 150–2500, normalised and tempered, hardness held in the 156–207 HB band. Every lot with EN 10204 3.1/3.2 MTC. ISO 9001:2015, made in Mumbai, India — exported to 50+ countries.
ASTM A182 F22 Class 3 · UNS K21590 · W.Nr. 1.73802¼Cr-1Mo — The Staircase's WorkhorseSteam + Hot Hydrogen DutyCarbon With a Floor — Creep Is Carbide StrengthStub Ends: A234 WP22 per B16.9½″–24″ NB · Classes 150–2500Pairs Certified TogetherEN 10204 3.1 / 3.2 · ISO 9001:2015
ASTM A182 F22 Lap Joint Flanges — Specifications at a Glance
What is an ASTM A182 F22 Lap Joint Flange?
The workhorse's backing flange. An ASTM A182 F22 lap joint flange is the loose backing ring of the two-piece system in 2¼Cr-1Mo alloy steel (UNS K21590) — chromium and molybdenum both doubled against the 1Cr grades, buying creep-rupture ratings at the hot end of the steam band and hydroprocessing's default hydrogen standing. The point on this pattern: the flange never touches the process, but it runs at line metal temperature — and it never welds, so it escapes the chrome-moly preheat/PWHT discipline. Per ASME B16.5, ½″–24″ NB, Classes 150–2500, normalised and tempered, Class 3 certified explicitly (no Class 2 exists), 156–207 HB; stub ends A234 WP22 per B16.9. EN 10204 3.1 on every lot.
Also searched as: F22 backing flange, F22 Class 3 lap joint flange, 2¼ chrome lap joint flange, A182 F22 LJ flange, chrome moly loose flange — all this page's product. Related pages: the lap joint hub (the pattern's full story), the carbon twins — A105 warm and LF2 cold — the staircase neighbours F11, F21 and F5, the F22 bench — weld neck / blind / long weld neck — and the alloy steel overview.
The Metal-Temperature Argument, at the Workhorse Rung
The argument at this rung has two halves: the heat reaches the never-wetted ring through the metal it clamps — at the hot end of the steam band, where even F11's allowable-stress column thins out while F22's keeps going — and where hydrogen rides along, the chromium earns its second salary on the Nelson curves. The ring can skip the welding; it cannot skip the temperature class.
A different mission — vanadium-modified precision creep strength for power-plant steam
The workhorse's honest advice runs both ways: duty inside F11's ratings gains nothing from F22's premium, and duty past F22's hydrogen chart names its reason and steps up to F21 — or, sulphur-driven, to F5. Descending honestly is engineering too.
What the Pattern Gives This Grade
Both Dials Doubled
Chromium roughly doubled and molybdenum doubled to a full 1% against the 1Cr grades — the combination that buys the higher creep-rupture ratings and the hydrogen-service standing that made F22 hydroprocessing's default.
The Weld-Procedure Dodge
The backing ring never welds — no preheat, no PWHT, no procedure to qualify or reopen on the flange. F22's discipline is stricter than F11's, milder than the high-chrome rungs' — and the ring dodges all of it.
The Class Certainty
Class 3 is the flange default — and no F22 Class 2 exists in A182 — purchase orders occasionally invent one, fuelled by the plate specification's numbering; our certificates state Class 3 explicitly.
The Workhorse's Stock
The most-stocked rung of the staircase — the volume that keeps F22 the most economical of the serious chrome-moly grades and usually the shortest alloy lead time, flange and WP22 stub end both.
Specification Notes — Getting F22 Lap Joints Right
Three honest notes.There is no Class 2: a specification saying 'F22 Cl.2' needs correcting at source — we quote Class 3 against it and say so; an unqualified 'F22' order is certified Class 3. These identifiers are F22's own: K21590, W.Nr. 1.7380 and the 0.87–1.13 molybdenum band migrate onto F21 datasheets in error — read the chromium band on every document. And the pattern's boundaries apply in any grade: heavy external loads, severe vibration and high-moment positions read the weld neck bench — most hydroprocessing joints are weld necks, and lap joints earn their place where hot lines dismantle; the hub page states the boundaries fully.
How Our F22 Lap Joint Flanges Are Manufactured
1
Material — certified A182 F22 Class 3 forgings, normalised and tempered with the condition and class stated and furnace records retained; heat-number transfer at the first operation.
2
Machining — B16.5 lap joint dimensions: OD, thickness, bolt circle to class; bore and shoulder turned to suit the stub end's lap.
3
Shoulder dressing — the radius dressed to bear evenly on the back of the lap — spreading bolt load instead of concentrating it.
4
Testing — hardness verified against the 156–207 HB band as the proof of proper tempering; chemistry certified per heat with the carbon floor proven — 0.05% minimum, because creep is carbide strength.
5
No welding, ever — the ring's whole career is mechanical: no weld, no preheat, no PWHT — the pattern's gift on an air-hardening 2¼-chrome grade.
6
Pairing & certification — matched to A234 WP22 stub ends where ordered; one EN 10204 3.1 document per pair (3.2 witnessed on request); packed sea-worthy with laps and shoulders protected.
Where F22 Lap Joint Flanges Are Used
Where the workhorse and the pattern meet: hydrotreater and hydrocracker loops — the grade's home ground — hot steam headers and boiler circuits at the top of the steam band, refinery hot utility systems, and petrochemical units that run F22 as their default hot-alloy spec — specifically the positions that earn a lap joint: exchanger and reactor-circuit connections that dismantle at every turnaround, spools rotated to distribute wear, and bolt circles that must align without pipe-twisting, where re-assembly never reopens a weld procedure. Production and supply below:
F22 Alloy Steel Stock — The Workhorse on the ShelfThe Two-Piece System — Flange, Stub End, Butt Weld, PipeAlloy Steel Supply — Protected Bores, Export Ready
F22 Lap Joint Flange Dimensions
Flange dimensions are class-governed per ASME B16.5 — identical in every grade; stub ends per B16.9. Full class-by-class charts:
Seven elements — the class matters most on this page:
1
Size & standard — e.g. 6″ NB ASME B16.5.
2
Pressure class — 150#–2500#.
3
The grade and class — an unqualified F22 is quoted and certified as Class 3; a specification saying ‘Class 2’ needs correcting at source — no F22 Class 2 exists.
4
Stub end — A234 WP22 matched pair with schedule and B16.9 type, or ‘flange only’.
5
The service — hot steam and hydroprocessing confirm F22; hydrogen past its curves steps to F21, sulphur-driven circuits to F5.
6
Certification — EN 10204 3.1 (our standard) / 3.2 witnessed, pairs certified together on one document.
Example: “Lap Joint Flange, 6″ NB, ASME B16.5 Class 600, ASTM A182 F22 Class 3, with A234 WP22 stub ends Sch 80 (B16.9 Type A, supplied together), pairs on one MTC, EN 10204 3.1 — 14 sets.” Quotations normally within 24 hours with price, unit weights (both parts) and delivery.
F22 Lap Joint Flanges — Frequently Asked Questions
What is an ASTM A182 F22 lap joint flange?
An ASTM A182 F22 lap joint flange is the loose backing flange of the two-piece lap joint system, forged in 2¼Cr-1Mo alloy steel (UNS K21590, W.Nr. 1.7380) — the chrome-moly staircase's workhorse, bought for creep-rupture ratings at the hot end of the steam band and for the hydrogen-service standing that makes it hydroprocessing's default grade. Like every lap joint flange it slides over the pipe, sits free behind the stub end's flared lap, and carries the entire bolt load without touching the line fluid — and because it never welds, it stays out of the chrome-moly weld discipline entirely; the joint's single butt weld belongs to the stub end. Manufactured per ASME B16.5 in ½" to 24" NB, Classes 150 to 2500, normalised and tempered, Class 3 quoted and certified explicitly, with EN 10204 3.1/3.2 certification on every lot.
How does the two-piece lap joint system work?
By splitting sealing from bolting. The stub end butt-welds to the pipe: its flared lap provides the gasket face and does all the fluid contact. The backing flange never welds and never wets: it slides on before the stub end is welded — the classic site lesson — spins freely until the bolts enter, and transmits bolt load through its radiused shoulder onto the back of the lap. Two consequences follow on this grade. First, the flange's material follows its own duty — here temperature, which is why the ring is F22 rather than plain carbon steel on hot steam and hydrogen circuits. Second, the chrome-moly consequence: the flange never welds, so it never enters the weld procedure — no preheat, no PWHT on the ring itself; the joint's single butt weld belongs to the stub end. The full pattern story — stub end types, the alloy economy, the honest boundaries — is on the lap joint hub page.
Why must the never-wetted backing flange still be F22 — the metal-temperature argument?
Because the backing flange gets hot even though it never gets wet — the argument that runs the whole lap joint bench, here at the workhorse rung. The heat reaches the ring through the metal it clamps: bolted hard against the lap of a hot steam header or a hydroprocessing circuit, the flange sits at essentially line metal temperature — past the territory where plain A105 is trusted (above roughly 425°C carbon steel's ratings carry the graphitisation caveat), and at the hot end of the steam band where even F11's allowable-stress column thins out while F22's keeps going. Add hydrogen and the chromium earns its second salary: F22's Nelson-curve standing covers hot hydrogen duty that would attack a leaner steel's carbides. The ring can skip the welding; it cannot skip the temperature class. F22 backing F22 is the normal answer, and the certificate proves both halves.
What is the chemical composition of ASTM A182 F22?
Carbon 0.05-0.15% (a deliberate range with a minimum — see the carbon FAQ), manganese 0.30-0.60%, silicon ≤0.50%, chromium 2.00-2.50%, molybdenum 0.87-1.13%, phosphorus ≤0.040%, sulphur ≤0.040%. Two identity marks against the 1Cr grades below it: chromium roughly doubled, and molybdenum doubled to a full 1% — the combination that buys both the higher creep-rupture ratings and the hydrogen-service standing. And one mark worth checking in the other direction: these identifiers are F22's own — K21590, W.Nr. 1.7380 and the 0.87-1.13 molybdenum band migrate onto F21 datasheets in error, as that grade's page explains. Chemistry is verified per heat and travels on the EN 10204 3.1 MTC.
What are the mechanical properties of F22 lap joint flanges?
In the Class 3 normalised-and-tempered condition A182 requires tensile strength 515 MPa (75 ksi) minimum, yield strength 310 MPa (45 ksi) minimum and elongation 20% minimum, with hardness controlled in the 156-207 HB band — the strongest certificate of the low-chrome creep family, a full step above F11's 485/275. As with the whole family, the room-temperature numbers understate the purchase: F22 is bought for its creep-rupture ratings at the hot end of the steam band, where the allowable-stress tables separate it decisively from the 1Cr grades. For the backing-flange duty the strength arrives as margin: the ring works in bolting and bending at line metal temperature, and the B16.5 rating tables for the grade's material group carry it. The hardness band is the mill's proof of proper tempering — floor and ceiling both. Supplied with the condition and class stated and records retained.
Why does F22's carbon have a minimum?
Because creep strength is carbide strength — the logic that runs the whole low-alloy staircase. F22's job is to resist slow deformation over years at the hot end of the steam band, and the mechanism is a dispersion of chromium-molybdenum carbides pinning the microstructure: no carbon, no carbides, no creep resistance. So the specification writes carbon as a range with a floor, 0.05-0.15% — the mill must prove there is enough carbon to form the strengthening phase, not just little enough to weld. The floor sits at 0.05 rather than F11's 0.10 because 2¼Cr steel builds its carbides efficiently enough to afford it, keeping weldability in hand for the stub end's butt weld. A datasheet printing F22 carbon as '≤0.15' has lost the floor — and the point. On a lap joint order the floor travels on both certificates: the flange's and the matched stub end's together.
What are F22 Class 1 and Class 3 — and why is there no Class 2?
F22 comes in exactly two classes, and the numbering skips: Class 1 is the annealed, lower-strength condition — maximum weldability and softness, appearing mainly in fittings practice — while Class 3, the flange default, is normalised and tempered to 515 MPa tensile / 310 MPa yield. There is no F22 Class 2 in A182; the designations carried over from historical plate practice (A387 Grade 22 Classes 1 and 2 exist, which fuels the confusion), and purchase orders occasionally invent an 'F22 Cl.2' that no standard defines. If a specification reaching you says Class 2, it needs correcting at source — we quote Class 3 against it and say so. An unqualified 'F22' order is quoted and certified Class 3. The lap joint wrinkle: the backing ring never welds, so Class 1's weldability advantage buys nothing here — one more reason Class 3 is the bench's answer.
What stub ends pair with F22 lap joint flanges?
The matching stub end is wrought 2¼Cr-1Mo per ASME B16.9 in ASTM A234 WP22 — the fitting grade that pairs with F22 forgings exactly as WP11 pairs with F11 and WP5 with F5, sharing the chemistry philosophy and welded to the pipe with the line's qualified chrome-moly procedure, preheat and PWHT included. That butt weld is the joint's only weld, and it belongs entirely to the stub end: the backing flange never enters the procedure. The matching rules are the pattern's usual dimensional ones — lap OD to the flange's shoulder, schedule to the line bore — plus the documentary one: flange and stub end bought as a matched pair and certified together on one EN 10204 document, class and carbon floor stated on both sides, so the '2¼ chrome both halves' answer is provable at handover. Where an order needs B16.9 Type A or Type B lap details, state it and the pair is machined to suit.
Does an F22 backing flange need preheat and PWHT?
No — the backing flange never welds, so it never needs either. F22's welds take the chrome-moly discipline in earnest: 2¼Cr steel air-hardens firmly, and code work runs qualified procedures, preheat, controlled interpass and post-weld heat treatment on every joint — stricter than F11's regime, milder than the high-chrome rungs'. The lap joint backing flange inherits none of it, because it is never welded to anything: it slides over the pipe, floats behind the lap, and does its whole job mechanically. The discipline concentrates instead on the joint's single butt weld — stub end to pipe, A234 WP22 to the line, welded once under full control and returned by PWHT toward the certificate's hardness band. On hydroprocessing turnarounds this matters twice: fewer alloy welds to make and test in the first place, and a flange that can be swapped, rotated or re-used without any weld procedure being reopened. The dodge covers the flange, not the joint — the stub end's weld takes the full discipline, always.
Where does F22 sit on the chrome-moly staircase?
On the second step, and it is the workhorse — the most-stocked, most-specified rung of the family. The staircase climbs by chromium: F11 at 1¼% opens the creep bench for steam and moderate hydrogen; F22 at 2¼% doubles both alloying dials for the hot end of the steam band and hydroprocessing hydrogen duty — the default answer for a huge share of hot alloy piping; F21 at 3% nominal steps deeper into the Nelson curves where F22's hydrogen headroom runs thin; F5 at 4-6% is the first true sulphidation grade; F9 at 8-9.5% doubles that for the sourest heater service; and F91, the vanadium-modified 9-chrome, turns off toward precision creep strength for power-plant steam. Every rung has a lap joint page on this site, and the workhorse's honest advice runs both ways: duty inside F11's ratings gains nothing from F22's premium, and duty past F22's hydrogen chart names its reason and steps up. State the service and the rung picks itself.
What sizes and pressure classes do F22 lap joint flanges come in?
½" to 24" NB per ASME B16.5 in Classes 150, 300, 400, 600, 900, 1500 and 2500, with larger diameters machined to B16.47 or drawing — the full class-by-class lap joint dimension charts are on this site. The order book mirrors the grade's habitat: steam headers concentrate in Classes 300 to 600, with hydroprocessing circuits running Classes 600 to 1500 where hydrogen partial pressure climbs alongside temperature. Dimensionally an F22 lap joint flange is identical to any other grade's — B16.5 governs by class, not by material — so the charts serve every grade on the bench; what changes is the rating table behind the class, where the grade's material group keeps usable pressures at temperatures that retire carbon steel and stretch the 1Cr grades. As the family's most-stocked rung, F22 usually carries the shortest alloy lead times. State size, class and the stub-end question together, and our quotation returns price, unit weight and delivery per class.
How much does an F22 lap joint flange weigh?
Exactly what the same-size lap joint flange weighs in any other steel — B16.5 fixes the dimensions by class, and alloy density differences are negligible. Representative Class 150 figures for the flange alone: 1" roughly 0.8 kg, 2" roughly 2 kg, 4" roughly 5.5 kg, 8" roughly 14 kg, climbing steeply with class; the A234 WP22 stub end adds its schedule-dependent mass. The commercial difference sits in the metallurgy and the paperwork: F22 carries its alloy surcharge, controlled heat treatment and per-lot testing in its price — moderated by the workhorse's volume, which keeps it the most economical of the serious chrome-moly rungs — and the matched stub end carries its weld-end preparation in its own. Our quotations state unit and consignment weights per line item, flange and stub end separately, and the site's flange weight chart carries the full reference tables.
How are your F22 lap joint flanges manufactured?
As the pattern's standard sequence with the class discipline at the heat-treatment step. Certified A182 F22 Class 3 forgings are normalised and tempered — the condition and class stated on the certificate, with furnace records retained — then machined to B16.5's lap joint dimensions: OD, thickness and bolt circle to class, bore and shoulder turned to suit the stub end's lap, and the shoulder radius dressed to bear evenly on the back of the lap. Hardness is verified against the 156-207 HB band as the proof of proper tempering; chemistry is certified per heat with the carbon floor proven — 0.05% minimum, because creep is carbide strength. Heat-number marking transfers at the first operation. No welding is performed on the flange at any stage — the ring's whole career is mechanical. Where the order includes A234 WP22 stub ends, the pair is dimensionally matched and certified together on one EN 10204 3.1 document (3.2 witnessed on request). Packed sea-worthy with laps and shoulders protected.
What details are needed to get an accurate F22 lap joint flange quotation?
Seven elements plus commercial terms: (1) size and dimensional standard — e.g. 6" NB ASME B16.5; (2) pressure class — 150 to 2500; (3) the grade and class — an unqualified 'F22' is quoted and certified as Class 3; a specification saying 'Class 2' needs correcting at source, because no F22 Class 2 exists in A182; (4) the stub end — A234 WP22 matched pair with schedule and B16.9 type, or 'flange only'; (5) the service where it helps — it confirms the rung: duty past F22's hydrogen chart steps to F21, sulphur-driven circuits to F5; (6) certification — EN 10204 3.1 (our standard) or 3.2 witnessed, pairs certified together on one document; (7) quantity as pairs or pieces, and destination. Quotations normally return within 24 hours with price, unit weights for both parts, and delivery.
Who manufactures ASTM A182 F22 lap joint flanges in India?
Tesco Steel & Engineering is an ISO 9001:2015 certified flange manufacturer based in Mumbai, India, producing ASTM A182 F22 Class 3 lap joint (lapped joint) flanges per ASME B16.5 from ½" to 24" NB (larger to B16.47 or drawing) in Classes 150-2500 — each machined from certified 2¼Cr-1Mo forgings in the normalised-and-tempered condition, hardness-verified in the 156-207 HB band, carbon floor proven on every heat, with the shoulder dressed to bear evenly on the lap, heat-number marked, and certified to EN 10204 3.1/3.2 with the class stated explicitly. Matched A234 WP22 stub ends per B16.9 are supplied against the same order, pairs certified together on one document. Alongside the complete A182 F22 range — weld neck, slip-on, socket weld, threaded, blind, spectacle blind and long weld neck — the full chrome-moly staircase in every flange type, and the complete lap joint grade bench. Exported to more than 50 countries.